

As a supplier of Food Double Cone Mixers, I understand the importance of airtightness in these machines. In the food industry, the quality and safety of products are of utmost importance, and the airtightness of a mixer can significantly impact both. This blog post will explore the airtightness requirements of a Food Double Cone Mixer, why they are crucial, and how we ensure our mixers meet these standards.
Why Airtightness Matters in Food Double Cone Mixers
Product Quality
One of the primary reasons for maintaining proper airtightness in a Food Double Cone Mixer is to preserve the quality of the food products being mixed. When a mixer is not airtight, it can allow air, moisture, and contaminants to enter the mixing chamber. This can lead to oxidation, spoilage, and changes in the texture and flavor of the food. For example, in the case of powdered food products, exposure to air and moisture can cause clumping, which not only affects the appearance of the product but also its functionality.
Hygiene and Safety
Food safety is a top priority in the food industry. An airtight mixer helps prevent the entry of dust, bacteria, and other harmful substances into the food. This is especially important in a production environment where multiple batches of different products may be processed. Without proper airtightness, cross - contamination can occur, leading to potential health risks for consumers.
Regulatory Compliance
The food industry is highly regulated, and there are strict standards regarding the manufacturing and handling of food products. Many regulatory bodies require food processing equipment, including mixers, to meet certain airtightness requirements. Failure to comply with these regulations can result in fines, product recalls, and damage to a company's reputation.
Airtightness Requirements
Sealing Materials
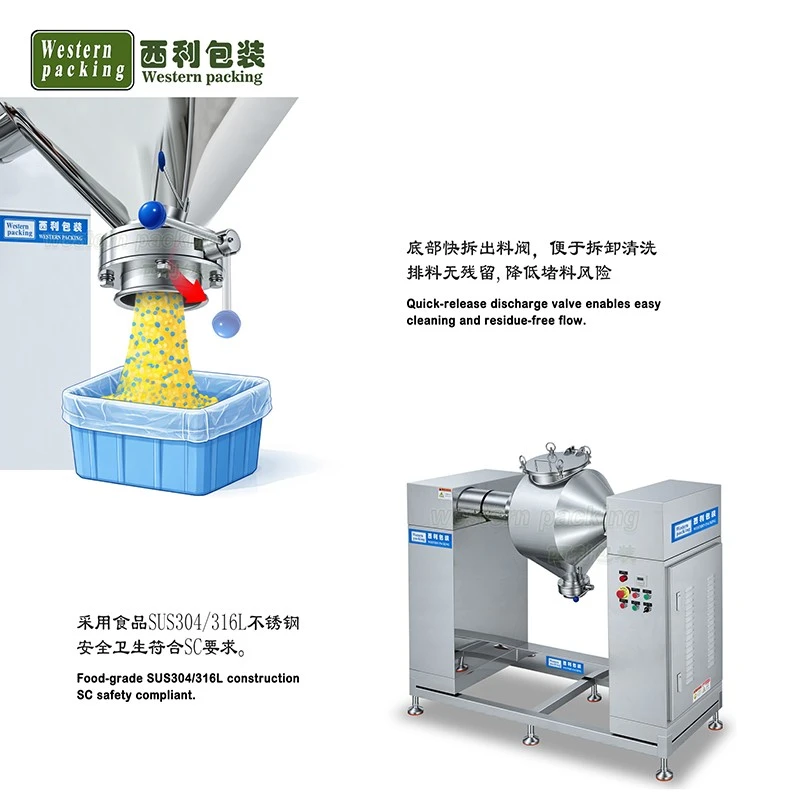
The choice of sealing materials is crucial in ensuring the airtightness of a Food Double Cone Mixer. These materials must be food - grade, non - toxic, and resistant to wear and tear. Common sealing materials used in our mixers include silicone and EPDM (Ethylene Propylene Diene Monomer) rubber. These materials have excellent sealing properties and can withstand the harsh conditions of food processing, such as high temperatures and exposure to various chemicals.
Design and Construction
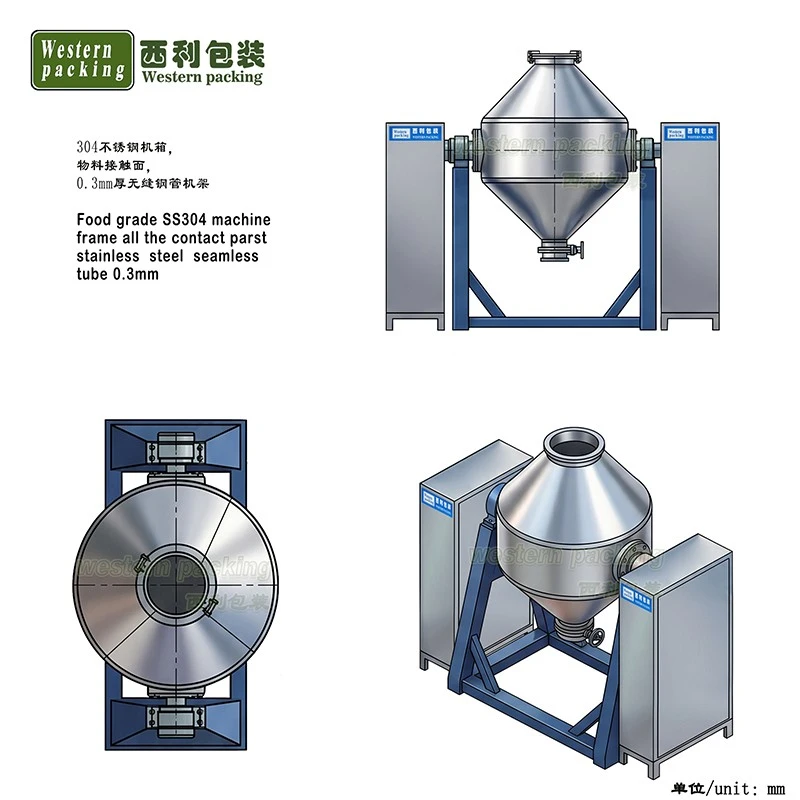
The design and construction of the mixer also play a significant role in its airtightness. Our Food Double Cone Mixers are designed with precision to minimize gaps and openings that could allow air or contaminants to enter. The joints and connections between different parts of the mixer are carefully engineered and sealed using advanced techniques. For example, the doors and access panels of the mixer are equipped with tight - fitting gaskets that create a secure seal when closed.
Pressure Resistance
In addition to preventing the entry of external air and contaminants, the airtightness of a Food Double Cone Mixer also needs to withstand the internal pressures generated during the mixing process. Our mixers are designed to handle the pressure changes that occur when the double cones rotate and the food materials are mixed. This ensures that the airtight seal remains intact throughout the operation, preventing any leakage.
How We Ensure Airtightness in Our Food Double Cone Mixers
Quality Control
At our company, we have a strict quality control process in place to ensure that every Food Double Cone Mixer meets the highest airtightness standards. Each mixer undergoes a series of tests before it is released to the market. These tests include pressure tests, leak detection tests, and visual inspections of the sealing components.
Continuous Improvement
We are constantly researching and developing new technologies and materials to improve the airtightness of our mixers. Our engineering team is always looking for ways to enhance the design and construction of the mixers to make them more airtight and reliable. For example, we are exploring the use of new sealing technologies that can provide even better performance in challenging food processing environments.
Customer Feedback
We value our customers' feedback and use it to improve our products. If a customer reports any issues related to airtightness, we take it seriously and work to resolve the problem as quickly as possible. We also use customer feedback to identify areas for improvement in our manufacturing processes and product design.
Applications of Airtight Food Double Cone Mixers
Baking Industry
In the baking industry, our Food Double Cone Mixer is used to mix various ingredients such as flour, sugar, and spices. The airtightness of the mixer ensures that the ingredients are well - mixed without being exposed to air or moisture, which can affect the quality of the baked goods.
Dairy Industry
For the dairy industry, our mixers are used to blend different dairy products and additives. The airtight environment helps maintain the freshness and flavor of the dairy products, preventing spoilage and contamination.
Snack Food Industry
In the snack food industry, our Cone Blender Mixing Powder and Grain is used to mix seasonings, powders, and grains. The airtightness of the mixer ensures that the flavors are evenly distributed and that the products remain fresh and free from contaminants.
Conclusion
In conclusion, the airtightness requirement of a Food Double Cone Mixer is of utmost importance for maintaining product quality, hygiene, and regulatory compliance. At our company, we are committed to providing high - quality mixers that meet these requirements. Our mixers are designed with the latest technologies and the best sealing materials to ensure optimal airtightness.
If you are in the food industry and are looking for a reliable and airtight Food Double Cone Mixer, we invite you to contact us for more information. Our team of experts will be happy to answer any questions you may have and help you find the right mixer for your specific needs. We look forward to the opportunity to work with you and contribute to the success of your food processing operations.
References
- Smith, J. (2018). Food Processing Equipment: Design and Operation. Wiley.
- Jones, A. (2019). Hygiene and Safety in Food Manufacturing. Elsevier.
- Food and Drug Administration. (2020). Current Good Manufacturing Practice in Manufacturing, Packing, or Holding Human Food.